By Liangyu Laser Technical Team | 15-min read
Hot Stamping Foil for Plastic: PP, PE, PET, ABS and Cosmetic Packaging
Table of Contents
Plastic foil performance depends on polymer type, surface energy, coating or treatment, part shape and production window. Test the foil grade on your real PP, PE, PET or ABS part before bulk production.
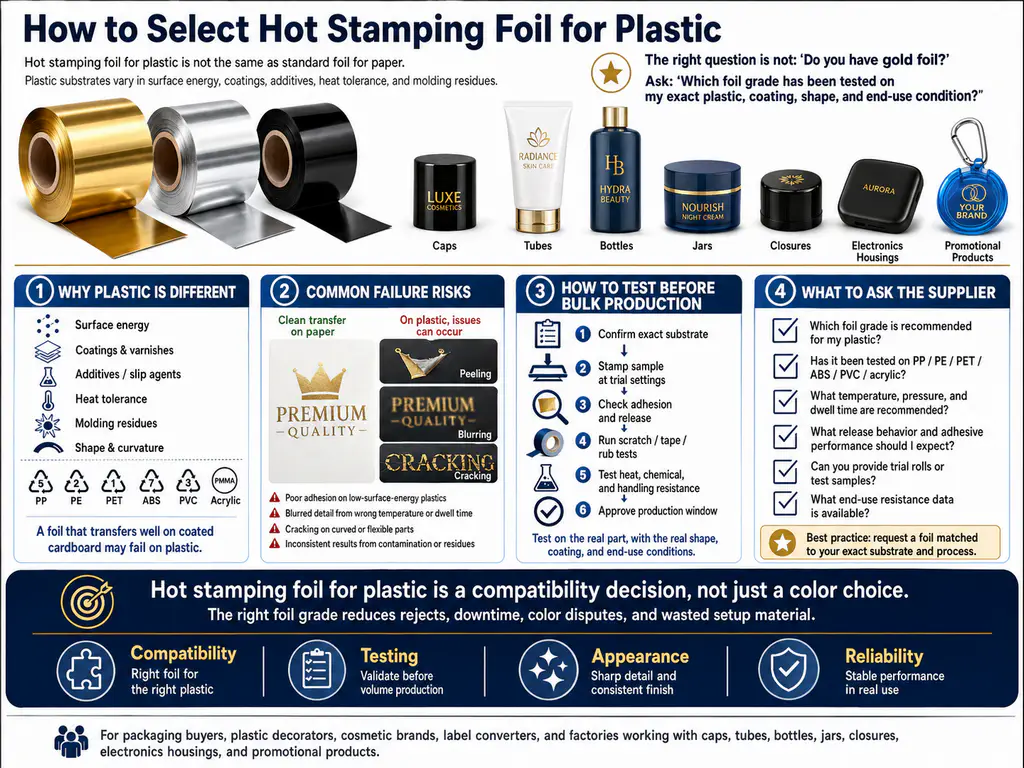
Hot stamping foil for plastic is not the same as standard foil for paper. Plastic surfaces have different surface energy, coatings, additives, heat tolerance, and molding residues. A foil that transfers cleanly onto coated cardboard may peel, blur, or crack on PP, PE, PET, ABS, PVC, acrylic, or cosmetic caps.
For buyers, the key question is not simply “Do you have gold foil?” The better question is: “Which foil grade has been tested on my exact plastic, coating, shape, and end-use condition?”
This guide explains how to select hot stamping foil for plastic, how to test it before bulk production, and what to ask a supplier before ordering. It is written for packaging buyers, plastic decorators, cosmetic brands, label converters, and factories working with caps, tubes, bottles, jars, closures, electronics housings, and promotional products.
What Makes Plastic Difficult to Foil Stamp?
Plastic is difficult because the surface may not naturally accept the adhesive layer of the foil. Some plastics are low surface energy materials, which means inks, coatings, and adhesives may not wet the surface well. Surface energy is also why dyne testing and corona or plasma treatment are common in plastic printing and converting.
Common plastic stamping challenges include:
- low surface energy on PP and PE,
- release agent or oil left from molding,
- curved or tapered parts that make pressure uneven,
- additives that migrate to the surface,
- coatings that soften under heat,
- plastic parts that deform when the die is too hot,
- poor matching between foil adhesive and resin type.
Plastic Substrate Compatibility Guide
The first step is identifying the resin and surface condition. “Plastic” is too broad for a useful foil recommendation.
| Plastic substrate | Typical use | Foil selection priority | Common risk |
|---|---|---|---|
| PP | cosmetic caps, closures, containers | high-adhesion foil, surface treatment | peeling or weak bond |
| PE | tubes, flexible packaging, bottles | treatment and flexible adhesion | poor wetting, rub-off |
| PET | bottles, labels, transparent packaging | clean transfer and heat control | distortion or weak edge detail |
| ABS | electronics, appliances, rigid parts | durable adhesion and scuff resistance | cracking on molded texture |
| PVC | cards, packaging, decorative parts | temperature control and compatible adhesive | surface damage or odor |
| Acrylic / PMMA | premium displays, cosmetic components | low-temperature testing, clean edge | crazing or heat marks |
Surface Treatment: The Step Buyers Often Miss
Many plastic stamping failures start before the foil ever touches the part. If the surface is not clean or receptive, the foil adhesive has nothing reliable to grip.
Surface preparation may include:
- wiping oil, dust, and mold release residue,
- corona treatment for films or sheets,
- plasma treatment for molded parts,
- flame treatment for selected plastic surfaces,
- primer or coating when required,
- controlled handling after treatment.
Corona treatment is widely used to raise the surface energy of plastic films and improve adhesion of inks, coatings, and adhesives. Enercon’s technical guide on corona treating gives a practical explanation of why treatment improves wettability.
One important detail: treatment can age. A plastic part treated weeks ago may not behave the same as a freshly treated part. If the job is high value, test the actual production lot, not only a clean lab sample.
How to Choose Hot Stamping Foil for Plastic
When selecting hot stamping foil for plastic, ask the supplier to match the foil to the resin, shape, finish, durability requirement, and stamping equipment. Avoid buying solely by color.
1. Match the Adhesive Layer to the Plastic
The adhesive layer is the part that bonds the color or metallic layer to the plastic. PP and PE often need stronger adhesion support than coated paper. ABS may accept foil more easily, but textured ABS still needs careful pressure control.
Ask whether the foil grade is designed for:
- PP or PE caps,
- PET bottles or labels,
- ABS appliance panels,
- PVC cards,
- acrylic cosmetic components,
- lacquered or UV-coated plastic.
2. Check Heat Tolerance
Plastic parts can warp, shrink, gloss-change, or show die marks if the temperature is too high. The right foil should transfer within a temperature range that the substrate can tolerate.
Start with supplier guidance, then test a low, middle, and high setting. Do not use a paper stamping temperature as the starting point for plastic.
3. Choose Release by Artwork
Large solid logos may need an easier release. Fine lines, QR-adjacent decoration, small text, and thin borders usually need sharper release control. If the foil releases too easily, edges may blur. If it releases too tightly, transfer may be incomplete.
4. Test Durability, Not Just Transfer
A sample can look perfect immediately after stamping and still fail after rubbing, alcohol exposure, oil contact, freezing, filling, transport, or customer handling.
For plastic packaging, test:
- tape adhesion after cooling,
- dry rub and wet rub,
- alcohol rub for cosmetic or fragrance packs,
- oil or lotion contact if relevant,
- scratch resistance,
- hot and cold storage,
- curved-area edge lifting,
- batch-to-batch color consistency.
Best Applications for Plastic Foil Stamping
Plastic foil stamping is used where a brand wants a premium metallic or pigment finish without labels or secondary decoration. It is common in:
- cosmetic caps, jars, tubes, and compacts,
- perfume closures and fragrance components,
- liquor caps and closures,
- electronics housings and control panels,
- plastic cards and membership cards,
- promotional products,
- rigid plastic packaging,
- medical or personal care components where approved materials are used.
Match the Foil to Part Geometry and End Use
Two parts made from the same resin may need different foil grades and tooling when their shapes, coatings and end-use tests are different. Review the real component geometry before approving a foil for production.
Short-Run Samples and Simple Artwork
Magnesium is often the practical starting point when the job is a prototype, a short run or a simple flat design. Confirm that the artwork does not require very fine detail and that the substrate will not cause rapid die wear.
Fine Detail and Repeat Production
Copper is a useful option when the design contains small text, fine lines or mixed solid and detailed areas. It offers better durability than magnesium, but the foil release and engraving depth still need to be tested together.
Long Runs, Embossing and Premium Packaging
Brass is usually considered for repeat production, demanding detail, deep engraving and foil-and-embossing work. Check the board, coating and pressure distribution before approving the tooling for a long production run.
Curved or Irregular Plastic Parts
Silicone tooling may help the die follow a curved or uneven surface. The part shape, heat tolerance, foil adhesive and contact pressure must be evaluated on the real molded component, not only on a flat sample.
Sampling Checklist Before Bulk Orders
Before approving hot stamping foil for plastic, test it under production-like conditions.
Use this checklist:
- Confirm the plastic resin: PP, PE, PET, ABS, PVC, acrylic, or blend.
- Test on the molded part, not only a flat plaque.
- Clean the surface exactly as production will clean it.
- Record whether corona, plasma, flame, or primer was used.
- Test the final artwork size, not only a simple square.
- Run at several temperatures and dwell times.
- Check adhesion after cooling.
- Rub test the stamped area.
- Test alcohol, oil, or lotion exposure when relevant.
- Inspect curved edges and raised areas.
- Keep the approved foil batch number and stamping parameters.
This documentation makes repeat orders easier and reduces blame between the buyer, molder, printer, and foil supplier.
Record the Trial Before Approving Bulk Production
A visual sample is not enough for repeat production. Record the material, treatment, foil batch and stamping window so the approved result can be reproduced when the order moves to another shift, machine or production lot.
| Record field | Information to keep |
|---|---|
| Plastic identification | Resin type, trade name, grade, color and molded-part lot |
| Surface condition | Coating, varnish, mold release residue and cleaning method |
| Pretreatment | Corona, plasma, flame or primer; record treatment date when relevant |
| Tooling | Die material, artwork size, solid-area size and part geometry |
| Foil | Supplier, foil grade, color, finish and batch number |
| Machine settings | Machine model, temperature, pressure, dwell time and speed |
| Immediate result | Coverage, edge definition, pinholes, gloss and visible part damage |
| Durability result | Tape adhesion, dry rub, wet rub, alcohol, oil or lotion resistance |
| Final decision | Approved, adjust and retest, or rejected; include the reason |
Questions to Ask Your Supplier
A serious supplier should ask about your plastic before recommending a foil. If the supplier never asks about resin type, coating, or surface treatment, the risk is on you.
Ask:
- Which plastic substrates has this foil grade been tested on?
- Does it work on untreated PP or PE, or is surface treatment required?
- What starting temperature range do you recommend?
- Is the foil suitable for curved or molded parts?
- Can it pass tape, rub, alcohol, or oil resistance tests?
- What roll width and core size are available?
- Can you slit sample rolls for trial production?
- How stable is the shade between batches?
- What storage conditions protect the foil before use?
Hot Stamping Foil for Plastic vs Labels, Pad Printing, and UV Printing
Hot stamping foil for plastic is best when the brand needs a clean metallic or pigment decoration directly on the part. It avoids label edges and can look more integrated than a sticker. However, it is not always the best choice.
Choose hot stamping when:
- the design is a logo, border, emblem, or decorative area,
- the surface can tolerate heat and pressure,
- the finish needs metallic brilliance,
- repeat production justifies tooling and setup,
- the decoration must look premium and permanent.
Consider labels, pad printing, screen printing, or UV printing when:
- the artwork has many colors,
- variable data is required,
- the surface shape is too complex,
- the plastic cannot handle heat,
- very small quantities do not justify tooling.
FAQ
Can I use paper hot stamping foil on plastic?
Usually not. Paper foil may transfer on some plastic samples, but it often lacks the adhesive system needed for PP, PE, PET, ABS, or coated plastic parts. Use a plastic-compatible foil grade.
Does hot stamping foil for plastic require corona or plasma treatment?
Sometimes. PP and PE often need surface treatment or a compatible coating. ABS and some coated plastics may stamp more easily, but testing is still required.
Why does foil peel off plastic after stamping?
Common causes include low surface energy, mold release residue, wrong foil adhesive, low pressure, low temperature, short dwell time, or poor cooling before adhesion testing.
What temperature should I use for plastic foil stamping?
There is no universal temperature. Start with the supplier’s recommended range, then test low, middle, and high settings on the actual plastic part. Watch for warping, gloss change, and edge blur.
Is hot stamping foil for plastic suitable for cosmetic packaging?
Yes, if the foil grade is matched to the plastic and tested for handling, alcohol, oils, lotions, and filling conditions. Cosmetic packaging should always go through durability testing before approval.
Related Technical Resources:
📞 Contact our technical team → — Quote turnaround in 24 hours.
Get a Plastic Foil Grade Recommendation
Send the resin grade, part photos, surface treatment, target finish, machine type and required resistance tests. LiangyuFoil will review the application and suggest a foil grade and sample plan for your production trial.